我們的粉碎機使用的標準錘子是雙端可逆型, 具有四個磨損邊緣. 當錘子鈍化到機器無法高效研磨的程度,或當錘子邊緣變得圓潤時, 旋轉錘子以使用新的鋒利邊緣. 一次應只轉動一排錘子,以免改變轉子平衡. 不要讓錘子磨損過多,否則會失去相對的兩個切割刃. 錘子可以通過磨機的維修門更換,同時錘軸可以通過磨機頂部兩側的維修門滑出, 或者通過主要維修門.
安裝在您的Schutte錘式磨機中的錘子在出廠時已經仔細平衡. 從我們工廠寄出的新套替換錘子也已仔細平衡並以排方式線接好. 每次操作時總是應只處理一排錘子,且不要將錘子從一排換到另一排. 粗心操作錘子可能會導致過度振動.
安裝說明: 以鐘錶法進行平衡
注意: 到達時, note that each row or stack of hammers are numbered on the top hammer. They are numbered 1-8.
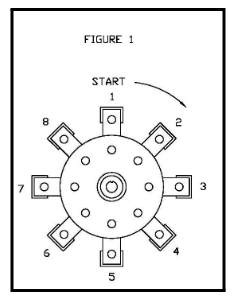
- Start with the row marked “1”. As illustrated in Figure #1, insert one hammer between every other disc. (In some cases, two hammers will be placed between each disc, depending on style of rotor).
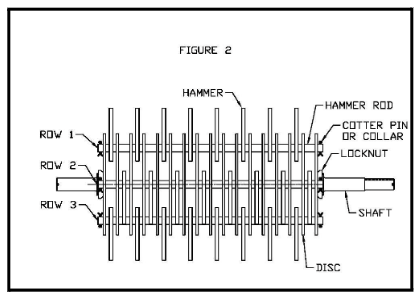
- Row 2 will follow with the hammers being staggered between the discs opposite the previous row. (See Figure #2)
- Continue installing the hammers in this manner working around the rotor in numerical order. (See Figure #1)
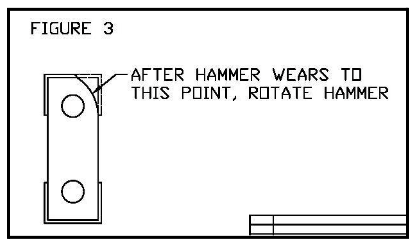
- Each hammer has four (4) wearing edges. Hammers should be rotated when the grinding edge wears to approximately half way between the hole and the original corner. Do not allow hammers to wear beyond this point or you will lose the ability to utilize all four edges. (See Figure #3)
- 建議當錘桿出現磨損跡象時更換錘桿 (一般而言的經驗法則是, 當錘的四個邊都使用過後更換整組錘桿). 在旋轉錘子時, 檢查錘桿本身是否過早磨損. 錘桿過度槽化表示需要更換.
- 在旋轉或更換錘子後,安裝套圈或開口銷於每支錘桿的末端.