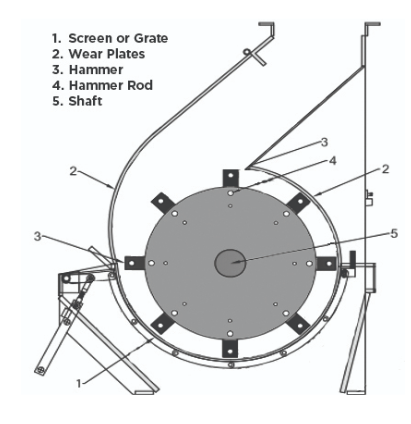
为更换做准备, 联系我们获取一套更换用的锤子. 每排锤子在工厂已按特定顺序布线并作为一组进行平衡. 在更换时必须保持锤子的顺序和这种平衡. 如果不这样做, 不平衡的锤子会引起过度振动.
旋转时: 遵循步骤 1 – 11 下面, 并在完成步骤之前旋转锤子堆以使用新的打击刃 12-15.
更换时: 新锤子是按组标记交付的 1 自 8. 将新锤子放入第X组 1 放入第X行 1, 如步骤中所述 12-15.
步骤:
- 关闭主电源断路器.
- 使用您现场的 OSHA 批准的锁定/挂牌程序固定主开关.
- 打开磨机罩.
- 从第一行开始
- 取下行的一端的套圈.
- 拉出杆,, 每释放一个锤子时, 取出锤子.
- 按杆上的顺序堆放每个锤子.
- 检查杆.
- 如果看到杆上有过度磨槽, 更换锤杆.
- 如果您正在更换锤子, 您还应更换锤杆.
- 从第X行开始 1. Insert one hammer between every other disc . (Some rotors use 2 hammers between each disc.)
- Insert the hammer rod to hold the hammer in position.
- Insert the next hammer and continue until all hammers for Row 1 are in place.
- Lock the rod, using the collar or cotter pin in the end of the rod.
- On Row 2, stagger the hammers between the discs opposite Row 1.
- Continue installing the hammers on the rods, working around the rotor in numerical order from Rows 3 through 8.
- After all the hammers have been re-installed, rotate the rotor by hand to ensure there are no catches.
- 关闭磨机罩.